
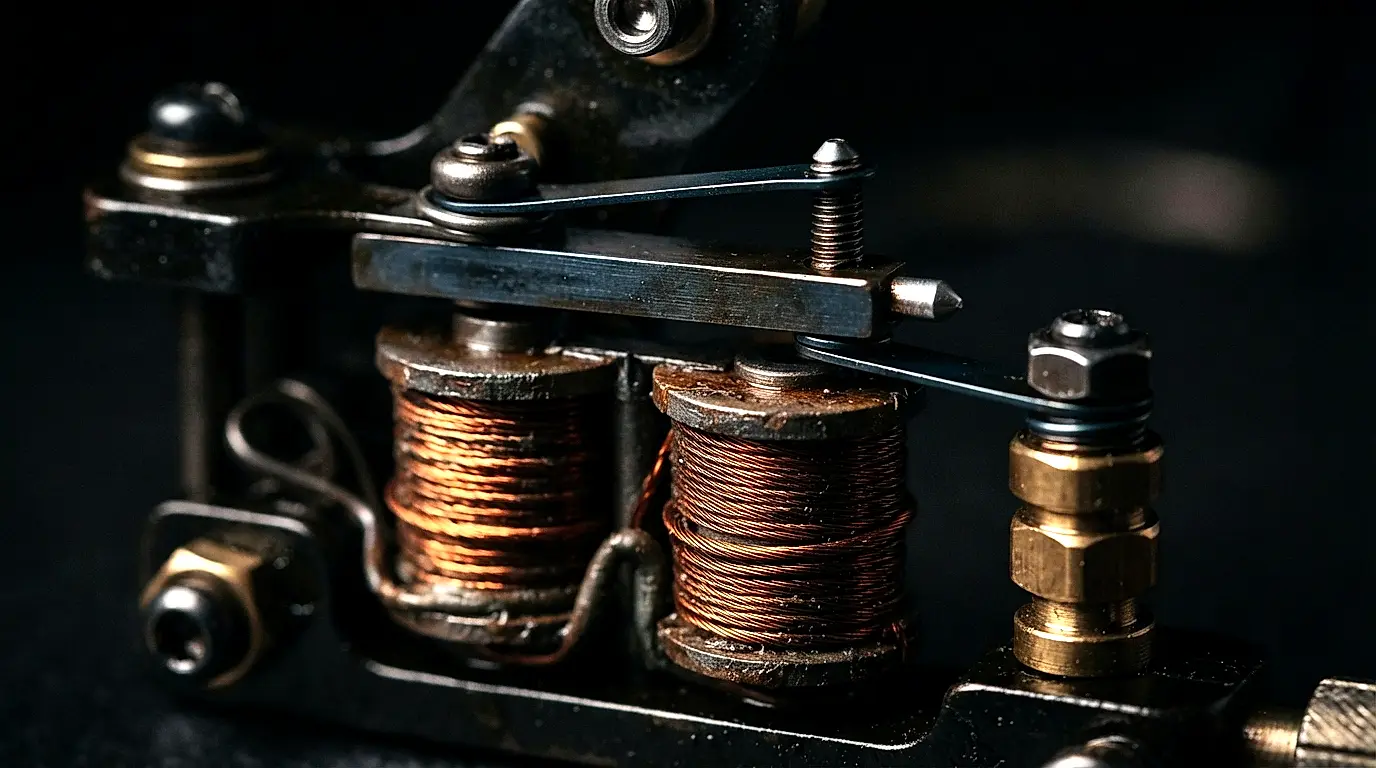
Coil, Rotary and Pen Drivetrains: Voltage, Give and Needle Dynamics

An engineering reference for the three tattoo machine drivetrain families: electromagnetic coil machines, which run as self-oscillating circuits at typically 80-120 Hz; permanent-magnet rotary machines with cam-driven strokes of 2.5-5.0 mm; and brushless pen drivetrains with PWM control and wide frequency ranges (one cited model: 25-140 Hz). Covers how voltage sets frequency, mechanical give (compliance), stroke and needle depth, and the electrical rules that apply in the EU and the US.
Tattoo machines are precision electromechanical transducers: they convert electrical power into controlled mechanical needle oscillation. Three distinct architectures dominate the market, each with fundamentally different physics. Coil machines are self-oscillating electromagnetic actuators; the armature bar, contact screw, capacitor, and spring form a resonant circuit whose frequency is voltage-tunable. Rotary machines are permanent-magnet DC motors driving a cam or eccentric; stroke is geometrically fixed by cam offset, and frequency tracks linearly with voltage. Pen machines use three-phase brushless DC motors with electronic commutation and PWM control; they have no brushes to wear and offer wide frequency ranges. Choosing between them is not a matter of brand preference but of understanding the engineering trade-offs: frequency range, torque under load, thermal dissipation, and mechanical compliance.
The key coupling parameter across all three families is give: mechanical compliance, how far the needle yields under force. Give acts as a mechanical low-pass filter: it absorbs sudden changes in skin resistance and needle impact, smoothing the force profile at the cost of some effective stroke. More give means the needle drives in less hard; less give means it hits harder and more precisely. Artists who understand give can tune it for the task: less give for crisp lining, more give for soft shading where tissue trauma must be kept low. Give is not a defect to eliminate, it is a design parameter to optimize.
Coil Machine Duty Cycles and Electromagnetic Dynamics
Coil machines are series-wound electromagnetic actuators operating in self-oscillating mode. When the power supply applies voltage, current flows through the coil windings, building a magnetic field in the laminated iron core. The field pulls the armature bar downward, compressing the front spring and driving the needle into the skin. At the bottom of the stroke, the armature breaks contact with the contact screw, interrupting current flow. The magnetic field collapses, the spring returns the armature to its resting position, and the contact re-establishes, completing one cycle.
- »Duty Cycle: The ratio of energized time to total cycle time, typically 40-60%. Tuned by capacitor value (0.22-0.47 µF in parallel with contacts) and spring tension (150-300 grams of force at the needle tip)
- »Inductance and Current Rise: Coil inductance (10-50 mH) and DC resistance (2-10 Ω) form an RL circuit. The time constant τ = L/R determines how fast current builds; typical τ = 1-25 ms. Higher voltage reduces the time to reach pull-in current, increasing frequency
- »Air Gap: The distance between the armature and coil core at rest, 0.5-1.5 mm. Smaller gaps increase magnetic force (force ∝ 1/gap²) but reduce stroke and increase the risk of residual magnetism holding the armature
- »Back EMF and Flyback Protection: When the contact opens, the collapsing magnetic field induces a voltage spike of 100-300 V across the coil. A flyback diode (1N4007) across the coil terminals shunts this spike to prevent contact arcing and coil insulation breakdown
- »Frequency Tuning: For a given spring tension and air gap, frequency increases approximately 10-15 Hz per volt applied. Capacitor value shifts the duty cycle: larger capacitance (0.47 µF) increases duty cycle, producing harder-hitting but slower strokes
Rotary Motor Torque and Cam Stroke Mechanics
Rotary machines use permanent-magnet DC motors (typically 5-20 mNm rated torque) coupled to a cam or eccentric pin. The cam converts continuous rotation into reciprocating linear motion; stroke length is geometrically fixed by the cam offset (eccentricity), typically 2.5-5.0 mm. Unlike coil machines where frequency is tuned by voltage and spring tension, rotary machines have a near-linear voltage-to-speed relationship: motor RPM increases approximately 500-800 RPM per volt at no load.
- »Speed-Torque Curve: Under needle load (1-3 N), motor speed drops 15-30% from no-load RPM. A motor rated at 6,000 RPM no-load at 12 V may run at 4,200-4,800 RPM when driving a 3.5 mm cam into skin
- »Force at the Needle: The cam turns motor torque into needle force. The peak available force is roughly the torque divided by the cam's eccentricity (half the stroke): a 10 mNm motor on a 3.5 mm stroke (1.75 mm eccentricity) can push up to about 5.7 N, above a 1-3 N needle load. A longer stroke gives less force from the same motor
- »Cam Profile Types: Circular eccentric cams produce sinusoidal motion (smooth, continuous), while heart-shaped or asymmetrical cams produce rapid advance with slower retraction (useful for color packing)
- »Bearing Life and Noise: Cam followers and motor bearings are small ball bearings that wear under radial load. Replace them at the manufacturer's interval or as soon as they get noisy; pitted cam surfaces cause audible grinding and frequency instability
- »Give Sources: Rotary machine give comes from motor shaft flex, bearing play, cam-to-follower clearance and needle bar bending. It is usually lower than in coil machines because the cam linkage is rigid
Brushless Pen Drivetrains and PWM Control
Pen-style machines use three-phase brushless DC (BLDC) motors with electronic commutation. Hall-effect sensors or back-EMF sensing detect the rotor position, and a microcontroller switches current through the stator windings in sequence, so there are no brushes to wear [10]. PWM (pulse-width modulation) at a 20-50 kHz carrier frequency controls motor speed, and motor speed sets the needle frequency. A linear actuator or scotch yoke mechanism converts the motor rotation to needle reciprocation.
- »Efficiency: brushless motors have no brush friction or brush wear. Coreless brushed micromotors reach up to about 90% at best too [2], so the real gains are less maintenance and less heat from brushes, which helps battery life in cordless pens
- »Commutation and Speed Control: The controller needs the rotor position to switch the windings. Sensored controllers read Hall-effect sensors; sensorless controllers read the back EMF on the unpowered winding [10]. Phase current is adjusted in real time to hold speed under varying skin loads
- »Give and Electronic Damping: Mechanical give in pen machines is usually the lowest of the three because the rigid drivetrain has few compliant elements. Some pens add electronic damping through current control, which absorbs load changes without adding mechanical compliance
- »Frequency Range: Pen machines cover wide ranges; one cited wireless pen is specified at 25-140 Hz [3], against typical figures of 80-120 Hz for coils and 60-100 Hz for rotaries. This range lets one machine handle lining, shading and colour packing
- »Thermal Management: Aluminium housings act as passive heat sinks. A pen that gets hot to hold is overdriven or failing; reduce the voltage and have it checked

Machine Tuning Protocol: From Power Supply to Skin
Systematic tuning ensures repeatable needle performance across sessions. Follow these steps for any new machine configuration before client work. All measurements assume a regulated DC power supply with ≤1% ripple and a digital tachometer or oscilloscope for frequency verification.
- 1Select machine type based on procedure: coil for traditional lining, rotary for smooth shading, pen for versatility across lining, shading and colour packing
- 2Set initial voltage on regulated power supply: coil 4-6 V, rotary 8-10 V, pen 10-12 V. Use the lowest voltage that achieves clean needle penetration, not the highest
- 3Adjust stroke length if your machine supports it: 2.5 mm for fine line work, 3.5 mm for general shading, 4.5-5.0 mm for heavy color saturation. Fixed-stroke machines skip this step
- 4Tune give by adjusting spring tension (coil) or needle bar compliance (rotary/pen): less give for crisp lining, more give for soft shading. Judge the result by test lines on practice skin
- 5Measure needle frequency with a tachometer aimed at the needle bar or an oscilloscope on the power leads: typically 80-120 Hz for coils and 60-100 Hz for rotaries; keep pens within the manufacturer's stated range. Adjust voltage to shift frequency
- 6For coil machines, verify duty cycle with an oscilloscope current probe: target 45-55% on-time. If below 40%, reduce capacitor value; if above 60%, increase capacitor or reduce spring tension
- 7Check temperature after 5 minutes of continuous dry running: the grip should stay comfortable to hold. If it gets hot, reduce voltage by 1-2 V; if it stays hot, have the machine serviced
- 8Inspect coil machine contact points: clean with isopropyl alcohol on a lint-free swab. Set contact gap to 0.5-1.0 mm using a feeler gauge. Replace contact screw if pitted or eroded
- 9Test on practice skin at your target voltage and frequency: adjust needle hang, stroke or give until lines go in cleanly and consistently, without blowouts. Verify across a 10-second continuous run
- 10Listen for mechanical anomalies during the 10-second test: irregular clicking in coil machines indicates contact bounce (increase spring tension); grinding in rotaries indicates bearing wear (replace bearings); high-pitched whine in pens indicates PWM frequency drift (recalibrate controller)
- 11Record all settings in a tuning log: machine model, voltage, measured frequency, stroke setting, spring tension/give, date, and any observations. Use the Machine Voltage Configurator tool for structured tracking
- 12After each session, clean and disinfect the machine as the manufacturer allows. Lubricate cam surfaces, bushings and O-rings only with the lubricant, and at the interval, that the manufacturer specifies

Common Errors and Failure Modes
These electromechanical failure modes directly impact needle performance and client safety. Most are detectable before they cause visible tattoo defects if the artist performs a pre-session tuning protocol.
- Coil Overheating — Overheating degrades winding insulation and increases copper resistance, causing frequency drift. Cause: excessive duty cycle (>70%) from an oversized capacitor or insufficient spring tension. Fix: reduce voltage by 1-2 V or replace the capacitor with a 0.33 µF value
- Rotary Motor Stall Under Load — Motor stops or stutters when the needle contacts skin, especially at low voltage on tough areas like palms. Cause: insufficient torque at operating voltage or needle drag in the tube or cartridge. Fix: increase voltage by up to 2 V, or replace the needle cartridge or tube
- Pen Frequency Instability — Needle speed varies erratically during a stroke, producing uneven ink deposition. Cause: controller calibration drift, Hall sensor misalignment, or voltage sag from an underpowered supply or weak battery. Fix: recalibrate the controller per the manufacturer's procedure; check that the supply or battery delivers the current the manufacturer specifies
- Contact Sparking in Coil Machines — Visible blue-white arcing at the contact screw indicates flyback voltage not being suppressed. Cause: missing or failed flyback diode, or contact gap too large. Fix: install 1N4007 diode across coil terminals (cathode to positive); reduce contact gap to 0.5 mm
- Excessive Needle Bounce — Needle impacts skin then rebounds before the next drive cycle, producing double-strikes and blurred lines. Cause: too much mechanical give or a spring resonance that matches the drive frequency. Fix: reduce give (tighten the spring or stiffen the needle bar); change to a spring with different stiffness to shift its resonance away from the drive frequency
- Noisy Rotary Operation — Audible grinding, clicking or whining during operation. Cause: worn bearings (pitted races), scored cam surface, or loose set screws on the eccentric. Fix: replace the bearings with the same size and type; polish the cam with 2,000-grit wet sandpaper; tighten all set screws with thread locker
- Pen Motor Vibration — Felt vibration in the handpiece that increases with frequency. Cause: unbalanced rotor, loose coupling between motor and yoke, or bent needle bar. Fix: have the rotor balanced or replaced; tighten coupling set screws; replace visibly bent needle bars
- Frequency Sag Under Load — Frequency drops significantly when the needle contacts skin compared with free air. Cause: a power supply that cannot deliver enough current, or high resistance in the wiring. Fix: use a regulated power supply rated for the current the machine needs; replace thin or damaged power cables
- Needle Hang on Retraction — Needle stays depressed after the drive stroke, failing to retract fully before the next cycle. Cause: insufficient spring return force (coil), cam follower binding (rotary), or yoke mechanism jamming (pen). Fix: increase spring tension; free the cam follower; clean and realign the yoke linkage
Regulatory Framework
The most common regulatory claim made about tattoo machines is wrong: they are not medical devices, so the medical-device standards frequently cited for them do not apply. What governs a tattoo machine is ordinary electrical-equipment law, covering product safety, electromagnetic compatibility and restricted substances. Studio licensing is a separate matter set locally, and it regulates the premises and the practitioner rather than the machine as a product.
- Tattoo machines are NOT medical devices under EU MDR 2017/745 [8]. Annex XVI extends the Regulation to certain products with no intended medical purpose, but it explicitly excludes tattooing products, so neither MDR classification nor IEC 60601-1 applies to the machine [8] [5]
- Electromagnetic compatibility is the requirement that does bite: the machine and its power supply must meet the EMC Directive 2014/30/EU [9], usually shown through a harmonised emission standard the manufacturer chooses for the product
- RoHS Directive 2011/65/EU restricts lead, mercury, cadmium and other hazardous substances in electrical and electronic equipment, and applies to the machine as an electrical product [12]
- A mains-powered power supply falls under the Low Voltage Directive 2014/35/EU, which covers 50-1000 V AC and 75-1500 V DC [13]; the machine itself runs on low-voltage DC, below that range
- FDA does not approve, clear or classify tattoo machines. Its published material on tattoos and permanent makeup addresses inks as cosmetics [7]
- UL 61010-1 is a safety standard for electrical equipment for measurement, control and laboratory use [6]. Where a manufacturer applies it to a tattoo power supply, that is a voluntary conformity choice rather than a federal requirement
- OSHA 29 CFR 1910 Subpart S governs electrical safety in the workplace [11], so it reaches the studio as a workplace rather than the machine as a product
Patrick's Note
"After years of watching artists plug in machines at whatever voltage the last person used, I will say this plainly: tuning is not optional. A 1-volt change on a coil machine shifts frequency by 10-15 Hz and completely alters needle penetration. A rotary motor running at 8 V instead of 10 V delivers about 20% less torque at the needle tip; your shading suddenly looks patchy and you blame the ink when it is the voltage. Brushless pens are even more sensitive: a 2% PWM drift can produce visible frequency ripple that ruins a smooth gradient. Treat your machine as the precision instrument it is. Measure voltage before every session. Record your settings. And if you have not replaced your contact screw or checked your bearing play in the last 500 hours, do it this week. For the latest in drivetrain engineering and field test reports, follow our Tech Watch journal at /blog/?category=Tech%20Watch"
Founder & Piercing Expert
Poli International
Common Questions
▸What is the purpose of this technical reference and why is its application critical for professional body art practitioners?
▸What are the typical electromechanical values that govern the operation of modern tattoo machine drivetrains?
▸What systematic steps should a technician follow to ensure a tattoo machine is properly tuned before beginning a procedure?
▸Why does a coil machine overheat during operation and what steps are necessary to rectify this electromechanical failure?
▸What causes a rotary machine motor to stall or stutter under load and how can this issue be corrected?
▸What specific regulatory frameworks and safety standards govern the classification and operation of tattoo machines in professional environments?
Anatomical Plates
Free Body Art Wall Posters
Print-ready reference posters for your studio or your own wall. Free to download and display, embed on your own site with attribution. Click any poster to preview it full size before downloading.
Page map · Electrical Engineering, Tattoo Machine Electromechanics
- Electrical Engineering, Tattoo Machine Electromechanics
- Critical Numbers
- Coil Machine Operating Voltage
- Rotary Machine Motor Torque
- Motor Efficiency
- Coil Machine Duty Cycles and Electromagnetic Dynamics
- Duty Cycle
- Inductance and Current Rise
- Air Gap
- Rotary Motor Torque and Cam Stroke Mechanics
- Speed-Torque Curve
- Force at the Needle
- Cam Profile Types
- Brushless Pen Drivetrains and PWM Control
- Efficiency
- Commutation and Speed Control
- Give and Electronic Damping
- Machine Tuning Protocol
- Select machine type based on procedure
- Set initial voltage on regulated power supply
- Adjust stroke length if your machine supports it
- Common Errors and Failure Modes
- Coil Overheating
- Rotary Motor Stall Under Load
- Pen Frequency Instability
- Regulatory Framework
- European Union
- United States
- Patrick's Note
- Related Topics
- Needle Geometry Physics
- Ergonomics in Body Art
- Journal
Built from this page's own sections, so it always matches what is below. It is a map of the page, not a set of claims, and carries no citations of its own.
Technical Specifications
| Parameter | Standard / Value |
|---|---|
| Coil Machine Voltage Range | 3-12 VDC |
| Coil Inductance | 10-50 mH |
| Coil DC Resistance | 2-10 Ω |
| Coil Duty Cycle (Operating) | 40-60% |
| Coil Operating Frequency | 80-120 Hz |
| Rotary Motor Torque | 5-20 mNm at 6-18 VDC |
| Rotary Cam Stroke Length | 2.5-5.0 mm |
| Rotary Speed Drop Under Load | 15-30% from no-load RPM |
| Motor Efficiency | Up to about 90% at best, coreless brushed [2]; model-dependent |
| Pen PWM Carrier Frequency | 20-50 kHz |
| Pen Needle Frequency | Manufacturer range; e.g. 25-140 Hz [3] |
| Give, Coil Machines | Highest (set by the spring) |
| Give, Rotary Machines | Lower (rigid cam linkage) |
| Give, Pen Machines | Lowest (rigid drivetrain) |
| Needle Depth | Set by needle hang and pressure, not stroke alone |
| Heat | Hot to hold = overdriven; see manufacturer limits |
| Back EMF Spike (Coil) | 100-300 V without flyback diode |
| Bearing Service Life | Manufacturer interval; replace when noisy |
Revision Deck
18 cards, taken directly from this page's specifications. Nothing here is generated: the deck is the same reviewed data as the table above. See the full table.
Printable wall chart (A4) — the critical numbers, the do-nots and the applicable standards on one page for the bench.
References
- [1]Liu P., Ouyang Y., Quan W. (2023) "Multi-Objective Optimization of a Long-Stroke Moving-Iron Proportional Solenoid Actuator." Micromachines 15(1):58, DOI 10.3390/mi15010058 (open access), electromagnetic force and stroke characteristics of solenoid actuatorshttps://pmc.ncbi.nlm.nih.gov/articles/PMC10818690/
- [2]maxon academy (2012): "maxon DC motor: Permanent magnet DC motor with coreless winding" (design and characteristics; coreless winding, no iron losses, efficiency up to over 90%)https://www.maxongroup.com/medias/sys_master/8803450421278.pdf
- [3]Cheyenne: SOL Nova Unlimited wireless machine, manufacturer technical page (BLDC drivetrain, 25-140 Hz, 2.5/3.5/4.0/5.0 mm stroke options)https://cheyennetattoo.com/en/tattoo-machines/sol-nova-unlimited
- [4]FK Irons: "Adjustable Stroke vs Fixed Stroke Tattoo Machines, When to Use Each" (manufacturer guide to stroke length and give)https://www.fkirons.com/blogs/official/a-comprehensive-guide-on-tattoo-machine-stroke
- [5]IEC 60601-1:2005/COR1:2006, Corrigendum 1 to "Medical electrical equipment, Part 1: General requirements for basic safety and essential performance". Retained for completeness only: this standard governs MEDICAL electrical equipment and does not apply to tattoo machines, which are not medical deviceshttps://webstore.iec.ch/publication/2611
- [6]UL 61010-1, Edition 3: Safety Requirements for Electrical Equipment for Measurement, Control, and Laboratory Use, Part 1 General Requirementshttps://www.shopulstandards.com/ProductDetail.aspx?productId=UL61010-1_3_S_20120511
- [7]US FDA: "Tattoos & Permanent Makeup" consumer information page. FDA regulates tattoo inks as cosmetics and does not approve, clear or classify tattoo machineshttps://www.fda.gov/cosmetics/cosmetic-products/tattoos-permanent-makeup
- [8]Regulation (EU) 2017/745 (Medical Device Regulation). Annex XVI extends the Regulation to listed products having no intended medical purpose, but EXPLICITLY EXCLUDES tattooing products, so tattoo machines are not medical devices in the EUhttps://eur-lex.europa.eu/eli/reg/2017/745/oj
- [9]Directive 2014/30/EU (EMC Directive): electromagnetic compatibility of electrical and electronic equipmenthttps://eur-lex.europa.eu/eli/dir/2014/30/oj
- [10]Gamazo-Real J.C., Vazquez-Sanchez E., Gomez-Gil J. (2010) "Position and Speed Control of Brushless DC Motors Using Sensorless Techniques and Application Trends." Sensors 10(7):6901-6947 (open access)https://pmc.ncbi.nlm.nih.gov/articles/PMC3231115/
- [11]OSHA 29 CFR 1910 Subpart S: Electrical Safety Standards for Workplaces.https://www.osha.gov/laws-regs/regulations/standardnumber/1910/1910SubpartS
- [12]RoHS Directive 2011/65/EU: Restriction of Hazardous Substances in Electrical Equipment.https://eur-lex.europa.eu/eli/dir/2011/65/oj
- [13]Directive 2014/35/EU (Low Voltage Directive): electrical equipment designed for use with a voltage rating of 50-1000 V AC or 75-1500 V DChttps://eur-lex.europa.eu/eli/dir/2014/35/oj
Put Science Into Practice
This technical standard is the architectural foundation for our professional analytical tools.