
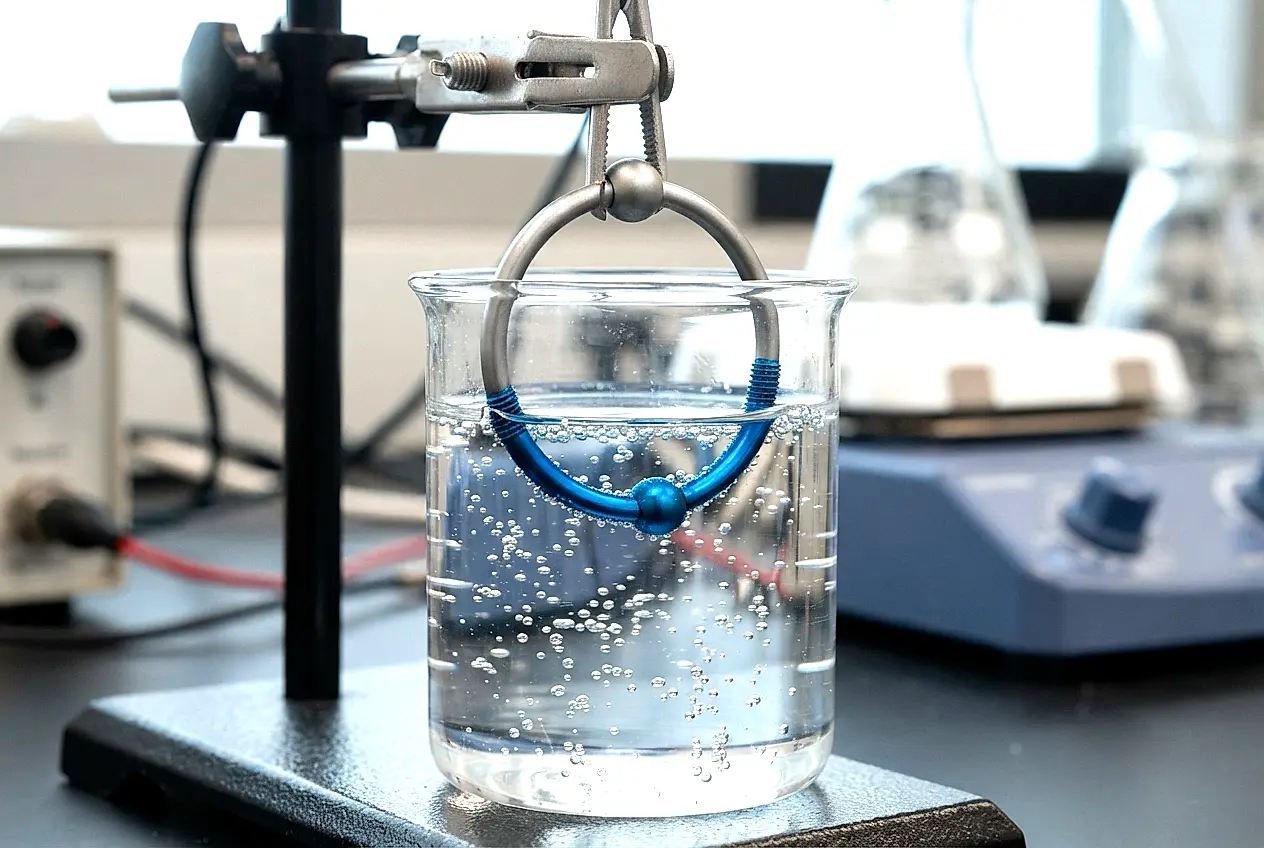
Thin-Film Interference & Titanium Oxide Science

Anodization is the electrochemical process that creates both the colour and the enhanced corrosion barrier on titanium body jewelry. This reference covers the thin-film optical interference physics that produce colour without pigment, the electrochemistry of titanium oxide growth, voltage-to-colour mapping, how colour anodizing differs from other anodizing, durability limitations in the body environment, and quality verification methods.
Interactive · Live Physics
Anodising Voltage Simulator
Drag the voltage. The colour is computed live from the thin-film interference equations in this article, not from a lookup table: oxide thickness grows at ~2.2 nm/V, and the reflected spectrum is resolved across 380-730 nm.
Simulated Type II result on clean Ti-6Al-4V ELI. Real-world colour shifts with surface prep, electrolyte and bath temperature, which is why colour alone never identifies a metal. poliinternational.com/wiki
Anodization is one of the most misunderstood processes in the body jewelry industry. The colours produced, golds, purples, blues, greens, look like paint or plating to the untrained eye, which has led to widespread confusion among clients and, frankly, among some practitioners. The reality is physically elegant: anodized colour is not a substance applied to the surface. It is light itself being manipulated by the thickness of an ultra-thin transparent oxide layer grown directly from the titanium surface. There is nothing to chip, nothing to flake, and nothing to release into the body, because there is nothing foreign present. The colour is pure physics.
For body jewelry, anodization serves two simultaneous functions. The first is aesthetic: it produces a range of vivid colours without dyes, pigments, or coatings that could introduce sensitising or toxic substances. The second is protective: the anodic oxide layer is a dielectric barrier that further passivates the titanium surface against the extremely mild corrosive environment of human tissue fluids. On implant-grade ASTM F136 titanium (Ti-6Al-4V ELI), the natural oxide layer is already among the most corrosion-resistant surfaces in clinical use [8]. Anodization thickens that layer many times over and makes it more uniform, which may improve biocompatibility further [1].
Thin-Film Optical Interference: Why It Produces Colour
The colour seen on anodized titanium is produced by thin-film optical interference, the same physical mechanism that produces colours in soap bubbles, oil films on water, and butterfly wings. Understanding this mechanism is essential to understanding why anodized colour behaves differently from paint.
- »The mechanism: White light (containing all visible wavelengths) strikes the anodized surface. Some light reflects from the air-oxide interface at the top surface. The rest transmits through the TiO₂ layer and reflects from the oxide-metal interface below. The two reflected beams recombine. For certain oxide thicknesses, specific wavelengths interfere constructively (amplified) while others interfere destructively (cancelled). The constructively amplified wavelength is the colour we see.
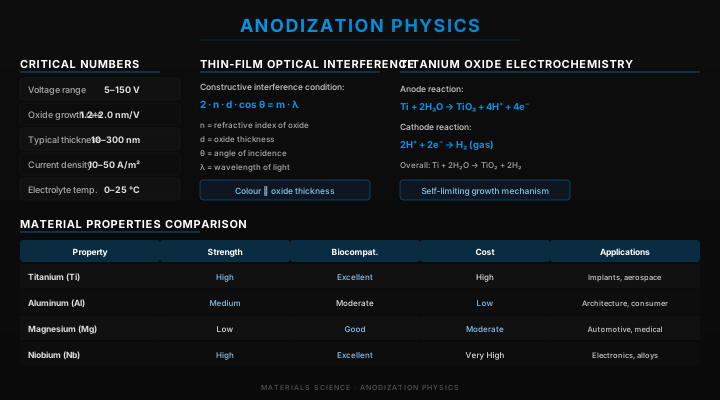
- »The colour condition: the colour depends on the optical path through the oxide (2nt, where n is the refractive index and t the thickness) compared with the wavelength of light. As the oxide thickens, the wavelengths that are reinforced or cancelled shift, so the colour changes through a repeating sequence [9].
- »Why there are no "pure" colours: The interference condition amplifies a range of wavelengths around the peak, not a single wavelength. This is why anodized blues have a slight violet quality and anodized greens tend toward teal. The spectral purity is physically limited by the refractive index contrast at the interfaces.
- »Voltage controls thickness: the oxide grows by about 1.4-2.8 nm per volt, depending on the electrolyte [1]. This near-linear relationship is why anodizing is controllable and reproducible within one setup.
- »Why a coating is different: paints, lacquers and PVD coatings can imitate the anodized look, but they are a separate layer added on top of the surface, not the metal's own grown oxide.
Titanium Oxide Electrochemistry
The electrochemical process of anodization involves oxidising the titanium surface in a controlled electrolyte bath using a direct current power supply.
- »At the anode (the jewelry piece): Ti → Ti⁴⁺ + 4e⁻. The titanium surface donates electrons to the circuit. Ti⁴⁺ ions react with oxygen ions from water in the electrolyte: Ti⁴⁺ + 2O²⁻ → TiO₂. This oxide forms directly at the metal surface and grows inward into the titanium, it is not deposited from solution.
- »At the cathode (counter electrode): 2H₂O + 2e⁻ → H₂ + 2OH⁻. Hydrogen gas evolves at the cathode. The cathode is typically a stainless steel plate.
- »Self-limiting growth: TiO₂ is a semiconductor with low ionic conductivity. As the oxide layer thickens, the electric field that drives further oxidation decreases. At a fixed applied voltage, oxide growth is self-limiting, the process naturally stops when field-driven ion migration through the oxide can no longer occur. This is why voltage (not time) controls final oxide thickness.
- »Surface preparation criticality: The oxide grows from the metal surface uniformly only if the surface is clean, polished, and free of contamination. Scratches, machining marks, grease, or oxide from previous heating create uneven oxide nucleation, visible as blotchy, inconsistent colour. Electrolytic polishing (electropolishing) before anodization is the standard preparation step for high-quality results.
- »Not the aluminium 'Type I/II/III': that classification (chromic acid, sulfuric acid, hard anodizing) belongs to aluminium anodizing. For titanium, AMS 2488 Type 2 is a thick grey anti-galling finish used in engineering; the colour anodizing used for body jewelry is a much thinner interference film [3].
Durability, Limitations, and Failure Modes
Anodized colour on body jewelry is inherently more durable than any coating, but it is not indestructible. Understanding its failure modes is essential for accurate client communication.
- »Mechanical abrasion: The TiO₂ layer, while chemically stable, has a hardness of approximately 5–6 Mohs, softer than quartz. Fine scratches from jewellery-on-jewellery contact, abrasive cleaners, or ultrasonic cleaners gradually remove the outer surface of the oxide, thinning the layer and shifting the interference colour (usually toward a thinner-layer, lower-voltage colour).
- »Chemical attack: Strong alkalis (pH > 12) and strong acids (pH < 1) can dissolve TiO₂. Body fluids range from slightly acidic (skin surface, about pH 5.5) to slightly alkaline (blood, about pH 7.4), which does not attack the oxide. However, repeated exposure to alkaline soaps, harsh cleaning chemicals, or prolonged soaking in saline at high temperature can gradually degrade the oxide surface.
- »Tongue piercing accelerated wear: The oral environment subjects jewelry to mechanical wear from tooth contact, food particles, and continuous movement, compounded by saliva (mildly acidic, enzymatically active). Anodized colour on tongue bars wears noticeably faster than on comparable jewelry in low-contact sites. Clients should be advised that colour longevity at oral sites is measured in months, not years.
- »Re-anodization: Unlike plating, worn anodized jewelry can be stripped by the manufacturer and re-anodized to restore or change colour. The jewelry geometry is not affected provided the stripping time is controlled. This is a significant practical advantage over plated jewelry, which cannot be re-plated without specialist facilities.
- »UV stability: TiO₂ anodized colour shows excellent UV stability because the colour mechanism is physical (interference), not chemical (dye bleaching). Long-term UV exposure does not fade anodized jewellery.
Anodization Quality Verification Protocol
Steps for verifying anodization quality at point of purchase or at studio intake before use.
- 1Step 1, Visual uniformity check: Examine the jewelry under a bright directional light (not fluorescent diffuse lighting). The colour should be uniform across all surfaces with no blotchy areas, streaks, or colour transitions that do not follow the piece geometry. Blotching indicates surface contamination prior to anodization.
- 2Step 2, Colour consistency check for matched sets: For jewelry sets (e.g., labret + nostril studs intended to match), compare pieces side by side under identical lighting. Colour should match within one visible shade. Significant variation between pieces from the same "batch" indicates poor voltage control during anodization.
- 3Step 3, Scratch test (non-destructive zone): Using a metal tool on an area that will not be visible when worn, lightly drag across the surface. Anodized colour should not flake, chip, or peel. If any coating lifts away as a film or flake, it is not anodized, it is painted or lacquered, and must not be used as body jewelry.
- 4Step 4, Verify base material certification: Anodization quality is dependent on the substrate. Request the manufacturer's material certificate confirming ASTM F136 (Ti-6Al-4V ELI) or ASTM F67 (Grade 1/2/4 commercially pure Ti) [5] [6]. Anodization on non-implant-grade titanium alloys, or on steel plated to look like titanium, is not acceptable.
- 5Step 5, Ultrasonics protocol: If ultrasonically cleaning anodized titanium, use a mild, pH-neutral cleaning solution only. Alkaline ultrasonic solutions (pH > 9) will gradually degrade the oxide surface. Limit ultrasonic cleaning time to 2–3 minutes per cycle for anodized pieces, extended ultrasonic exposure accelerates surface wear.
- 6Step 6, Post-sterilization inspection: after autoclaving, inspect anodized pieces for colour shift. Heat can change some anodized colours slightly; set aside any piece whose colour shifts strongly and report it to the supplier.
- 7Step 7, Client communication: Advise clients that anodized colour is integral to the metal surface and will not chip or flake. It will gradually lighten (shift toward thinner-layer colour) with mechanical wear over months to years depending on placement and care. This is normal, not a defect.

Critical Errors
Common anodization and jewelry specification errors with consequences for safety and client outcomes.
- Confusing anodization with plating when advising clients — Clients ask "will the colour come off?" A practitioner who says "yes, eventually, like paint" is technically wrong. The colour is structural interference, not a coating. It changes by surface thinning (lightens/shifts), not flaking. This distinction matters for informed consent and client trust.
- Accepting plated-to-look-like-titanium jewelry from discount suppliers — Gold-plated, PVD-coated, or lacquered jewelry that mimics anodized titanium visually but is not made from implant-grade titanium base metal is not acceptable for body art use. Plating can chip, releasing substrate metal particles into the wound. The scratch/chip test (Step 3 above) is essential.
- Ultrasonically cleaning anodized jewelry in alkaline solution — A common sterilization error. Alkaline ultrasonic cleaning solutions are formulated for stainless steel, not titanium. Regular use on anodized pieces causes progressive oxide degradation that affects both colour and corrosion resistance.
- Assuming all "titanium" is implant grade — Titanium alloys include Grade 5 (Ti-6Al-4V) and Grade 23 (Ti-6Al-4V ELI, the implant grade covered by ASTM F136), as well as alloys not intended for implants. "Titanium jewelry" without ASTM F136 material documentation is unverified [5]. Anodization cannot convert substandard titanium into safe jewelry.
- Trying to reach a lower-voltage colour by re-anodizing — anodizing only adds oxide, so a piece can be taken to a higher-voltage colour but never back to a lower one. Going back needs the old oxide stripped first, which is a job for the manufacturer.
- Using anodized jewelry in fresh piercings as a colour preference without explaining wear expectations — High-wear placements (oral, genital, high-movement sites) will lose anodized colour within months. Clients who selected coloured jewelry specifically for the aesthetics of a fresh piercing should be advised that natural silver titanium may be more appropriate for long-term wear at these sites.
Standards Governing Anodization & Titanium Jewelry
Standards and rules relevant to anodized titanium body jewelry. Body jewelry is not a medical device in the EU or the US.
- ISO 5832-3 (Ti-6Al-4V) and ISO 5832-2 (unalloyed titanium): the ISO implant material standards. ASTM F136 [5] and ASTM F67 [6] are widely used in Europe as well. Anodizing on a certified substrate is the benchmark.
- EU REACH Regulation (EC) 1907/2006 Annex XVII Entry 27: Nickel release limits apply to all metallic jewelry in prolonged skin/mucous membrane contact [10]. Titanium naturally meets this without restriction, but this must be verified for titanium alloys containing nickel additives.
- ISO 10993-5, -10 and -12 (cytotoxicity, sensitisation, sample preparation) [7]: medical-device standards that some suppliers use to support biocompatibility claims; they are not a legal requirement for body jewelry.
- General Product Safety Regulation (EU) 2023/988, applying since 13 December 2024: consumer products, including body jewelry, must be safe, with technical documentation and traceability.
- ASTM F136-13(2021): Wrought Ti-6Al-4V ELI, the primary US reference for implant-grade titanium substrate [5]. Anodization performed on F136 material is the industry-accepted standard.
- ASTM F67-13(2017): commercially pure (unalloyed) titanium, Grades 1-4, an alternative substrate for body jewelry [6].
- No FDA rule for anodized body jewelry: body jewelry has no medical purpose and is not regulated as a medical device.
- No mandatory testing: there is no required pre-market test for anodized body jewelry in the US. Many manufacturers use ASTM F136 certificates and EN 1811 nickel-release tests as quality markers [5].
- Thailand: no rule specific to body jewelry or anodizing was confirmed; ASTM F136 material certificates are the usual quality evidence [5].
- Singapore: body jewelry is not a medical device or health product, so the HSA does not register it; general consumer product safety rules apply.
- Australia: no national standard specific to body jewelry was confirmed; body art is regulated by the states and territories.
- Common practice across the region: buyers ask for EU REACH Entry 27 nickel-release results and ASTM F136 certificates as a minimum [5].
Patrick's Note
"When I explain anodization to clients, I start with a simple statement: 'The colour you are looking at is light. There is no dye, no paint, no coating. We ran electricity through the titanium in a salt bath, and the physics of light interference did the rest.' The look on their face when they understand this is always the same, it is the look of someone who did not expect jewellery to be interesting. The science is genuinely beautiful, but the practical reality keeps me honest about its limitations. I have always told clients directly: in your tongue, this colour will shift within a year. In your nostril, it will last five years easily. The physics that creates the colour is also the physics that limits its durability. A thinner oxide layer, made at a lower voltage, is more susceptible to abrasion. A thicker layer, made at a higher voltage, is more durable but more susceptible to thermal shift in the autoclave. What I find most useful to emphasise is what anodization is NOT: it is not a coating that can release into your body, it is not an allergen, and it is not a safety compromise. It is the same biocompatible titanium surface underneath, with a controlled thickness of its own inert oxide. The colour is a benefit, not a risk. That distinction matters."
Founder & Piercing Expert
Poli International
Common Questions
▸What is the process of anodization and why is it significant for jewelry professionals?
▸What are the critical numerical parameters and voltage thresholds for achieving specific colors?
▸How is the electrochemical procedure for titanium anodization performed in a studio setting?
▸How does mechanical abrasion affect anodized jewelry and what can be done to prevent it?
▸Which chemical factors cause degradation of the oxide layer and how can errors be avoided?
▸What regulatory standards and material verification steps are required for anodized body jewelry?
Anatomical Plates
Free Body Art Wall Posters
Print-ready reference posters for your studio or your own wall. Free to download and display, embed on your own site with attribution. Click any poster to preview it full size before downloading.
Page map · Anodized Titanium Oxide Colour: Physics & Market Guide
- Anodized Titanium Oxide Colour
- Critical Numbers
- Voltage range
- Colour sequence
- Oxide
- Thin-Film Optical Interference
- The mechanism
- The colour condition
- Why there are no "pure" colours
- Titanium Oxide Electrochemistry
- At the anode (the jewelry piece)
- At the cathode (counter electrode)
- Self-limiting growth
- Durability, Limitations
- Mechanical abrasion
- Chemical attack
- Tongue piercing accelerated wear
- Anodization Quality Verification Protocol
- Step 1, Visual uniformity check
- Step 2, Colour consistency check for matched sets
- Step 3, Scratch test (non-destructive zone)
- Critical Errors
- Confusing anodization with plating when advising clients
- Accepting plated-to-look-like-titanium jewelry from discount suppliers
- Ultrasonically cleaning anodized jewelry in alkaline solution
- Standards Governing Anodization & Titanium Jewelry
- European Union
- United States
- ASEAN & Asia-Pacific
- Patrick's Note
- Related Topics
- Metallic Biocompatibility
- MIM Revolution, Aerospace Body Jewelry
- Anthropometry & Jewelry Sizing
Built from this page's own sections, so it always matches what is below. It is a map of the page, not a set of claims, and carries no citations of its own.
Technical Specifications
| Parameter | Standard / Value |
|---|---|
| Voltage Range | Up to about 100-120 V DC |
| Oxide Thickness Range | A few nm (natural film) to about 150-300 nm |
| Growth Rate | About 1.4-2.8 nm per volt, by electrolyte [1] |
| Oxide Composition | TiO₂ (titanium dioxide) |
| TiO₂ Refractive Index | High (well above glass); varies with structure |
| Colour vs Voltage | Alloy- and setup-specific; build a reference chart [4] |
| Process (body jewelry) | Colour anodizing, thin interference film |
| Electrolyte (typical) | Dilute TSP or ammonium sulfate, room temperature |
| Surface Hardness (TiO₂) | ~5–6 Mohs |
| Substrate Standard | ASTM F136 Ti-6Al-4V ELI (implant grade) [5] |
| UV Stability | Excellent, interference colour is not UV-degradable |
Revision Deck
11 cards, taken directly from this page's specifications. Nothing here is generated: the deck is the same reviewed data as the table above. See the full table.
Printable wall chart (A4) — the critical numbers, the do-nots and the applicable standards on one page for the bench.
References
- [1]Sul Y.T. et al. (2001) "The electrochemical oxide growth behaviour on titanium in acid and alkaline electrolytes." Medical Engineering & Physics 23(5):329–346.https://doi.org/10.1016/S1350-4533%2801%2900050-9
- [2]Lausmaa J. (1996) "Surface spectroscopic characterization of titanium implant materials." Journal of Electron Spectroscopy and Related Phenomena 81(3):343–361.https://doi.org/10.1016/0368-2048(95)02530-8
- [3]Aladjem A. (1973) "Anodic oxidation of titanium and its alloys." Journal of Materials Science 8(5):688-704.https://doi.org/10.1007/BF00561225
- [4]Wadhwani C. et al. (2018) "Colorizing titanium-6aluminum-4vanadium alloy using electrochemical anodization: developing a color chart." Journal of Prosthetic Dentistry 119(1):26-28.https://doi.org/10.1016/j.prosdent.2017.02.010
- [5]ASTM F136-13(2021), Standard Specification for Wrought Titanium-6Aluminum-4Vanadium ELI (Extra Low Interstitial) Alloy for Surgical Implant Applications.https://store.astm.org/f0136-13r21e01.html
- [6]ASTM F67-13(2017), Standard Specification for Unalloyed Titanium for Surgical Implant Applications.https://store.astm.org/f0067-13r17.html
- [7]ISO 10993-5:2009, Tests for in vitro cytotoxicity.https://www.iso.org/standard/36406.html
- [8]Rack H.J., Qazi J.I. (2006) "Titanium alloys for biomedical applications." Materials Science and Engineering C 26(8):1269–1277.https://doi.org/10.1016/j.msec.2005.08.032
- [9]Diamanti M.V., Del Curto B., Pedeferri M. (2008) "Interference colors of thin oxide layers on titanium." Color Research & Application 33(3):221-228.https://doi.org/10.1002/col.20403
- [10]EU REACH Regulation (EC) No 1907/2006, Annex XVII, Entry 27, Nickel restrictions.https://echa.europa.eu/substances-restricted-under-reach
- [11]Mathieu H.J. (2001) "Bioengineered material surfaces for medical applications." Surface and Interface Analysis 32(1):3-9.https://doi.org/10.1002/sia.995
Put Science Into Practice
This technical standard is the architectural foundation for our professional analytical tools.
Compliance Suite
Need documented proof your materials comply?
REACH Guard PRO analyzes supplier safety data sheets against six regulation datasets (EU 2020/2081, EU + UK SVHC, CLP CMR, BPR Article 95, nickel-release) and issues a verifiable compliance report. From €9.50 per check.
Certify your products →