
Metal Injection Moulding: Aerospace Engineering Meets Body Art

Metal Injection Moulding (MIM) sits between casting (affordable but porosity-prone) and CNC machining (precise but expensive). In 2014, Patrick Poli and his son Frédéric Poli, working with US sintering expert Dr. Robert Sandford, ran micro-MIM trials for body jewelry and produced 0.8 mm threads and thin-wall components in 316L stainless steel. This reference covers the MIM process, why density matters for fatigue at small sizes, what the 2014 trials achieved, and how hot isostatic pressing (HIP) closes the internal porosity that starts fatigue cracks.
Every piece of body jewelry that is cast rather than machined contains a compromise. Investment casting, the industry standard for complex shapes, introduces microporosity: tiny voids left where the molten metal could not fill the mould completely, or where gas evolved from the metal as it cooled. In jewellery worn on a finger, microporosity is an aesthetic concern. In a 14-gauge labret post with a 1.2 mm diameter thread, it is a structural failure waiting to happen. Threads snap. Thin sections crack under the bending loads of daily wear. Electropolishing can improve the surface but cannot close a void inside the metal.
Metal Injection Moulding was developed in the 1970s and is now used widely for small, complex metal parts in medical devices, aerospace and other industries. It answers one question: how do you produce geometrically complex metal components at volume, with material properties approaching wrought metal rather than casting? MIM combines the geometric freedom of plastic injection moulding with the material science of powder metallurgy [1][10]. In 2014, Patrick Poli and Frédéric Poli trialled it for body jewelry at the micro scale, producing threads down to 0.8 mm and walls thinner than 0.5 mm.
The MIM Process: Eight Steps from Powder to Jewelry
Metal Injection Moulding is a multi-stage process that requires coordination between the injection facility, the debinding facility and the sintering furnace. The 2014 Sandford-Poli trials showed that these stages do not all have to be under one roof.
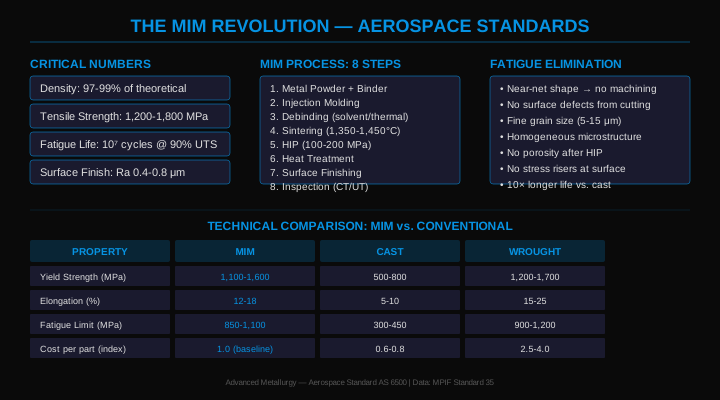
- »Step 1, Feedstock preparation: Fine metal powder (316L stainless steel, particle size 5–20 μm) is mixed with a thermoplastic binder system (typically paraffin wax + polyethylene + surfactant) at 55–65% metal volume fraction. The resulting compound pellets have the flow characteristics of a thermoplastic and the metal content of a casting.
- »Step 2, Injection moulding: The feedstock is heated to 150–180°C and injected into a precision steel mould under 40–150 MPa injection pressure. The mould geometry defines the final part shape. Shrinkage allowance (typically 15–20%) must be built into the mould dimensions. The injected "green part" contains the full geometric complexity of the final piece but is mechanically fragile.
- »Step 3, Solvent debinding (primary): The green parts are immersed in a solvent bath (typically heptane or acetone at 40–60°C) that selectively dissolves the paraffin wax binder component. This creates an interconnected pore network through which the remaining binder can be removed in the next stage. The "brown part" after solvent debinding is extremely fragile, individual labret posts and belly bars in this state will snap under finger pressure.
- »Step 4, Thermal debinding (secondary): The brown parts are heated in a controlled atmosphere furnace (< 600°C) to pyrolyse the remaining polymeric binder. The pore network from solvent debinding allows binder decomposition products to escape without building internal pressure that would fracture the part.
- »Step 5, Sintering: The debound parts are placed in a sintering furnace at 1,300–1,380°C in a reducing atmosphere (hydrogen or dissociated ammonia for 316L stainless steel). At sintering temperature, the metal powder particles bond by solid-state diffusion, the material transitions from a porous powder compact to a dense polycrystalline metal. The part shrinks uniformly by ~15–20% as porosity closes.
- »Step 6, Hot Isostatic Pressing (HIP): For the most demanding applications, sintered parts are subjected to HIP: high temperature and high isostatic gas pressure (typically 100-200 MPa, via argon) applied at the same time. HIP closes internal porosity that is not connected to the surface, bringing density close to that of wrought metal [7].
- »Step 7, Surface finishing: As-sintered parts have Ra ~0.8 μm, adequate for many industrial applications but not for body jewelry. Parts are electropolished to Ra < 0.1 μm, producing the mirror-bright, low-roughness surface body jewelry needs. Electropolishing also removes the surface oxide layer from sintering, revealing the clean chromium-rich passive layer of the 316L alloy.
- »Step 8, Quality verification: Dimensional inspection (thread gauge, diameter, length). Material testing (density by Archimedes method; tensile test samples from batch). Surface roughness measurement. Biocompatibility certification per ISO 10993 framework. The 2014 trials used US-based sintering facilities managed by Dr. Robert Sandford for steps 5–6, demonstrating the outsourced model.
Why MIM Eliminates Fatigue Failure at Microscale
The structural failure mode that MIM addresses is fatigue fracture, the progressive crack propagation that occurs when a material is subjected to repeated cyclic stress below its ultimate tensile strength. In body jewelry, cyclic stress occurs with every movement of the pierced anatomy: a tongue bar flexes thousands of times per day, a navel bar bends with every step. Cast components with internal microporosity contain stress concentrators, points where cracks start at far lower stress than in void-free material.
- »Microporosity as crack initiator: internal voids in cast metal concentrate stress under cyclic loading. The stress concentration factor at a spherical void is about 2, so the local stress is roughly twice the nominal stress. A small flaw under doubled stress, cycled thousands of times per day, can start a fatigue crack that grows until the cross-section can no longer carry the load.
- »Thread root geometry: thread roots are inherently stress-concentrating: the V-shaped valley of a thread concentrates stress by a factor of about 3-5 over the nominal stress in the threaded section. In a cast 316L labret with a 1.2 mm thread, casting porosity at the thread root adds to that geometric concentration, a plausible reason why cast internals snap.
- »MIM solution: well-sintered MIM parts have little internal porosity, and HIP closes most of what remains [7]. Thread roots in a HIP-treated MIM part are close to sound metal, with fatigue resistance approaching wrought 316L stainless steel.
- »HIP evidence: the effect of HIP on internal porosity is well documented in the materials literature [7]. NASA now publishes guidance on strength, fatigue and fracture control for additively manufactured spaceflight hardware (NASA-HDBK-5026, 2024) [2], where the same porosity questions arise.
- »Comparison to CNC machining: CNC-machined implant-grade titanium (ASTM F136) is the benchmark for high-value body jewelry and has no casting porosity. HIP-treated MIM 316L approaches machined 316L in mechanical properties, at a lower per-part cost for complex geometries.
The 2014 Sandford-Poli Trials: What Was Actually Achieved
The 2014 Thailand trials were not a proof-of-concept for MIM in general, which has been in industrial use since the 1970s. They tested the specific application of micro-MIM to body jewelry geometry: thin walls, small thread diameters, and the surface finish body jewelry needs.
- »The problem being solved: investment casting of 316L stainless steel body jewelry is limited in wall thickness and thread diameter, and porosity in thin sections and threads leads to micro-fractures and thread failures.
- »The breakthrough: the trials used a MIM feedstock formulated for fine geometry, injected on the equipment at the Thai factory used for the 2014 trials. With debinding and sintering outsourced to Dr. Robert Sandford's US facility, they produced components with 0.8 mm threads, wall thicknesses below 0.5 mm, and geometries previously achievable only by CNC machining.
- »The commercial model: a complete in-house MIM facility (injection moulding, debinding, sintering, HIP) is a large capital investment. The trials demonstrated a practical alternative: produce green parts on existing injection equipment and outsource debinding and sintering to a specialist facility, which greatly reduces the capital needed while keeping the metallurgical benefits of MIM.
- »What was NOT claimed: The 2014 trials established feasibility and demonstrated first-sample production quality. Full production-scale validation, including long-run process stability, consistent post-sintering dimensions across large batches, and full ISO 10993 biocompatibility certification of the specific feedstock-sinter combination, represents the next stage of development. This is the honest engineering position: the proof-of-concept is complete; production-scale implementation requires further investment.
- »Industry significance: To the knowledge of the participants, the 2014 trials were the first successful micro-MIM application to body jewelry geometry anywhere in the world. The body jewelry industry has since begun to explore MIM more broadly, but commercially available MIM body jewelry at sub-1 mm thread diameters remains rare as of 2026.
Evaluating MIM Body Jewelry Quality
How to assess whether body jewelry marketed as MIM actually meets the manufacturing quality implied by that claim.
- 1Step 1, Request the material certificate: MIM 316L stainless steel for body jewelry should carry a material certificate confirming alloy composition within ASTM F138 limits [4], plus the measured density and the surface roughness after electropolishing. Without these documents, the MIM claim cannot be verified.
- 2Step 2, Ask whether HIP was performed: MIM without HIP leaves some residual porosity; HIP brings density close to wrought metal [7]. For fine threads under daily cyclic loading, HIP is the safer specification. A supplier who does not know whether HIP was applied has not bought to that specification.
- 3Step 3, Dimensional verification of claimed geometry: Thread diameter (measured with calibrated thread gauge), internal bar length (measured with digital calipers), wall thickness at thin sections. MIM should reproduce dimensions within ±0.3% after sintering shrinkage compensation, consistency across multiple pieces from the same batch is the quality indicator.
- 4Step 4, Surface roughness check: Under a 10× loupe, the surface of correctly electropolished MIM 316L should appear mirror-bright with no visible porosity, pitting, or surface texture. Visible surface pores indicate either insufficient sintering density or inadequate post-processing.
- 5Step 5, Thread engagement test: MIM-produced threads at 0.8–1.2 mm diameter should engage smoothly with matching internal or external thread components. Rough engagement, binding, or visible burrs at thread roots indicate either dimensional error or insufficient debinding, binder residue in thread geometry is a known MIM defect mode.
- 6Step 6, Compare price point to process cost: Full-specification MIM 316L with HIP, electropolishing, and dimensional certification costs significantly more per piece than standard cast jewelry. If MIM jewelry is priced at the same level as standard cast pieces, the cost structure does not support genuine full-process MIM production. Due diligence is warranted.

Critical Errors
Specification and procurement errors in MIM body jewelry sourcing and use.
- Accepting "MIM" labelling without process verification — "MIM" as a marketing term has appeared on jewelry that may have been produced by conventional casting with cosmetic surface treatment. Without a verifiable material certificate, density measurement, and process documentation, the MIM claim is unsubstantiated.
- Purchasing MIM jewelry without HIP specification — MIM without HIP is denser than casting but not yet at wrought-equivalent properties. For body jewelry with fine threads under daily cyclic loading, HIP is the specification that most reduces the risk of fatigue failure.
- Assuming all 316L is equivalent regardless of manufacturing process — Cast 316L, MIM 316L (no HIP), MIM 316L (with HIP), and wrought 316L all have the same chemical composition but fundamentally different mechanical properties due to their respective microstructures. Chemical composition certification is necessary but not sufficient for structural quality assessment.
- Using MIM feedstock compatibility as a proxy for jewelry quality — the feedstock used in MIM affects both the sintering process and the final material properties. Feedstocks not designed for micro-geometry can produce parts that meet dimensional requirements but have lower density or poorer sintering. The feedstock specification should be part of the material documentation.
- Not distinguishing micro-MIM (body jewelry scale) from standard MIM — The challenges of MIM at sub-1 mm thread diameters are qualitatively different from standard industrial MIM at 5–10 mm dimensions. Suppliers with general MIM capability may not have successfully solved the specific geometric challenges of body jewelry scale. The 2014 trials specifically addressed this distinction.
Standards Governing MIM Body Jewelry
Material and product-safety rules that apply to MIM body jewelry. Body jewelry is not a medical device in the EU or the US.
- ISO 5832-1: wrought stainless steel for surgical implants, the ISO composition reference; ASTM F138-19 [4] is widely used in Europe as well. MIM 316L body jewelry should meet one of them for composition.
- EU MDR 2017/745: body jewelry, MIM or not, is not a medical device; Annex XVI point 2 covers implants that modify anatomy "with the exception of tattooing products and piercings". Words such as "implant-grade" describe the material, not a device.
- EU REACH Annex XVII Entry 27: nickel release limits apply whatever the manufacturing process: 0.2 μg/cm²/week for posts inserted into pierced parts of the body. 316L contains nickel, so every MIM 316L product must be tested (EN 1811), not assumed to pass.
- ISO 10993-5, -10 and -12: biological evaluation standards for medical devices. For MIM 316L, test data should come from the specific feedstock and process, because binder residue is a possible toxicological variable [9].
- General Product Safety Regulation (EU) 2023/988, applying since 13 December 2024: body jewelry must be safe, with technical documentation and traceability; process records (feedstock, sintering, HIP, finishing) are useful evidence.
- ASTM F138-19: The primary US reference for 316LVM stainless steel composition and property requirements [4]. MIM-produced 316L body jewelry should meet F138 for composition; density and mechanical properties should be verified by supplier.
- MPIF Standard 35: Metal Powder Industries Federation standard for MIM material properties. Specifies minimum density, tensile strength and elongation for MIM 316L [3].
- ISO 10993-1: the biocompatibility evaluation framework for medical devices, which some suppliers also use for body jewelry.
- FDA: body jewelry has no medical purpose and is not regulated as a medical device.
- Thailand: no rule specific to MIM body jewelry was confirmed; buyers in regulated markets usually ask for material certificates and nickel-release test results.
- ISO 13485:2016: the quality management standard for medical device manufacturers [8]. Body jewelry is not a medical device, so it is not required, but some manufacturers use it as a model for process control.
- Singapore: body jewelry is not a medical device or health product, so the HSA does not register it; general consumer product safety rules apply.
Patrick's Note
"In 2014, Frédéric and I set up what I believe was the first serious attempt to apply Metal Injection Moulding to body jewelry geometry at the micro scale. We had spent years watching cast components fail, threads snapping in tongue bars, thin sections cracking in internally threaded jewelry, and understanding why. The porosity from investment casting was the fundamental problem. The geometry we needed for implant-grade internals, sub-millimetre threads, walls below half a millimetre, was simply not achievable at consistent quality with traditional casting. We contacted Dr. Robert Sandford because he had the sintering expertise we needed. The injection side we could do ourselves, we had injection moulding capability already. What we needed was a sintering partner who understood the specific thermal profiles and atmosphere controls required for 316L at the density we were targeting. What Robert brought was not just the furnace, it was the metallurgical knowledge of what happens at the powder particle interfaces during sintering, and how HIP completes what sintering starts. The 0.8 mm thread result was the number I remember most clearly. That was not achievable with any casting method we had seen. Achieving it with MIM proved that the geometry ceiling we had been working under was a process ceiling, not a physics ceiling. The body jewelry industry can produce components at aerospace structural quality. What it currently lacks is the supply chain infrastructure and the commercial will to demand it consistently. The trials proved feasibility. The next step is production-scale implementation. That work is ongoing."
Founder & Piercing Expert
Poli International
Common Questions
▸What is Metal Injection Moulding and why is it significant for piercing professionals?
▸What are the critical engineering benchmarks and technical thresholds for MIM jewelry?
▸What are the specific steps involved in the MIM manufacturing procedure?
▸How does microporosity lead to fatigue failure and how can it be avoided?
▸How does binder residue affect thread quality and how is it evaluated?
▸Which regulatory requirements and standards govern the production of MIM body jewelry?
Anatomical Plates
Free Body Art Wall Posters
Print-ready reference posters for your studio or your own wall. Free to download and display, embed on your own site with attribution. Click any poster to preview it full size before downloading.
Page map · MIM Revolution in Aerospace Body Jewelry Explained
- MIM Revolution in Aerospace Body Jewelry Explained
- Critical Numbers
- MIM density
- Minimum thread diameter achieved (2014 trials)
- Wall thickness achieved (2014 trials)
- The MIM Process
- Step 1, Feedstock preparation
- Step 2, Injection moulding
- Step 3, Solvent debinding (primary)
- Why MIM Eliminates Fatigue Failure at Microscale
- Microporosity as crack initiator
- Thread root geometry
- MIM solution
- The 2014 Sandford-Poli Trials
- The problem being solved
- The breakthrough
- The commercial model
- Evaluating MIM Body Jewelry Quality
- Step 1, Request the material certificate
- Step 2, Ask whether HIP was performed
- Step 3, Dimensional verification of claimed geometry
- Critical Errors
- Accepting "MIM" labelling without process verification
- Purchasing MIM jewelry without HIP specification
- Assuming all 316L is equivalent regardless of manufacturing process
- Standards Governing MIM Body Jewelry
- European Union
- United States
- ASEAN & Asia-Pacific
- Patrick's Note
- Related Topics
- Metallic Biocompatibility
- Anodization Physics
- Needle Geometry Physics
Built from this page's own sections, so it always matches what is below. It is a map of the page, not a set of claims, and carries no citations of its own.
Technical Specifications
| Parameter | Standard / Value |
|---|---|
| MIM Theoretical Density Achieved | Approaching full density with HIP [7] |
| MIM Density (no HIP) | Typically about 96–99% [10] |
| Minimum Thread Diameter (2014) | 0.8 mm, believed to be a first for micro-MIM body jewelry |
| Minimum Wall Thickness Achieved | < 0.5 mm |
| Surface Finish (as-sintered) | Ra < 0.8 μm |
| Surface Finish (electropolished) | Ra < 0.1 μm |
| HIP Conditions (316L) | 900–1,100°C at 100–200 MPa argon pressure |
| Sintering Temperature (316L) | ~1,300–1,380°C in hydrogen atmosphere |
| Sintering Shrinkage | ~15–20% linear |
| Metal Powder Particle Size | 5–20 μm |
| Metal Volume Fraction (feedstock) | 55–65% by volume |
| Tooling Life (steel mould) | Typically hundreds of thousands of cycles |
| Primary Material (2014 trials) | 316L stainless steel MIM compound |
| Research Collaboration | Patrick Poli / Frédéric Poli + Dr. Robert Sandford (sintering), 2014 |
Revision Deck
14 cards, taken directly from this page's specifications. Nothing here is generated: the deck is the same reviewed data as the table above. See the full table.
Printable wall chart (A4) — the critical numbers, the do-nots and the applicable standards on one page for the bench.
References
- [1]German R.M., Bose A. (1997) Injection Molding of Metals and Ceramics. Metal Powder Industries Federation. ISBN 978-1878954619.https://www.mimaweb.org/Resources/Publications.aspx
- [2]NASA-HDBK-5026 (2024), Guidance on strength, fatigue and fracture control for additively manufactured spaceflight hardware.https://standards.nasa.gov/standard/nasa/nasa-hdbk-5026
- [3]MPIF Standard 35: Material Standards for Metal Injection Molded Parts (current edition). Metal Powder Industries Federation.https://www.mpif.org/
- [4]ASTM F138-19, Standard Specification for Wrought 18Chromium-14Nickel-2.5Molybdenum Stainless Steel Bar and Wire for Surgical Implants.https://store.astm.org/f0138-19.html
- [5]Heaney D.F. (ed.) (2012) Handbook of Metal Injection Molding, Part I: processing (feedstock, moulding, debinding, sintering). Woodhead Publishing. ISBN 978-0857090669.
- [6]Igharo M., Wood J.V. (1985) "Compaction and sintering phenomena in titanium-nickel shape memory alloys." Powder Metallurgy 28(3):131-139.https://doi.org/10.1179/pom.1985.28.3.131
- [7]Atkinson H.V., Davies S. (2000) "Fundamental aspects of hot isostatic pressing: an overview." Metallurgical and Materials Transactions A 31(12):2981–3000.https://doi.org/10.1007/s11661-000-0078-2
- [8]ISO 13485:2016, Medical devices: Quality management systems.https://www.iso.org/standard/59752.html
- [9]ISO 10993-12:2021, Biological evaluation of medical devices: Sample preparation and reference materials.https://www.iso.org/standard/75769.html
- [10]Heaney D.F. (ed.) (2012) Handbook of Metal Injection Molding. Woodhead Publishing. ISBN 978-0857090669.https://doi.org/10.1533/9780857096234.2.254
- [11]Upadhyaya G.S. (2002) Powder Metallurgy Technology. Cambridge International Science Publishing. ISBN 978-1898326397.
Put Science Into Practice
This technical standard is the architectural foundation for our professional analytical tools.