The Engineering of Density: Why 99% is Not Enough
In my 2014 research alongside Dr. Robert Sandford, we aimed to solve a problem that has plagued the body jewelry industry for decades: micro-porosity. Traditional investment casting, while suitable for decorative jewelry, is fundamentally incapable of reaching the structural densities required for medical implantation.
This article details the transition to Metal Injection Moulding (MIM) and why it remains the only viable path for high-performance body art engineering.
See our flagship MIM Revolution Wiki for full historical data.
1. The Porosity Problem in Traditional Casting
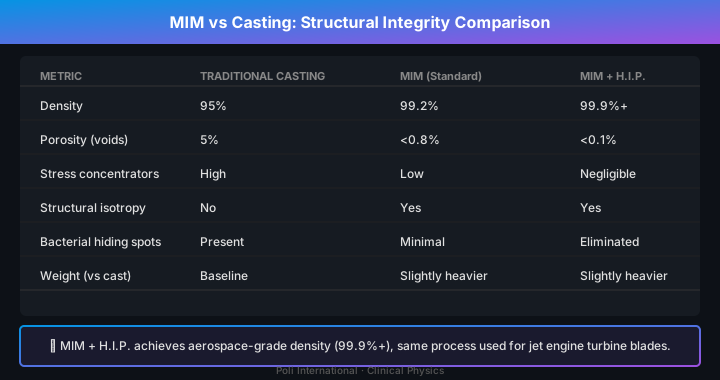
In a standard casting environment, molten metal is poured into a mold. As the metal cools and solidifies, gases become trapped, and the material shrinks unevenly. This results in "porosity"—microscopic voids or "bubbles" within the metal.
2. The MIM Solution: Forging from the Inside Out
MIM utilizes a fine metallic powder mixed with a binder material. This "green" body is then sintered in a high-vacuum furnace. Unlike casting, where gravity does the work, sintering uses thermal energy to fuse the particles at the atomic level.
3. The Role of H.I.P. (Hot Isostatic Pressing)
For our flagship aerospace-grade components, we don't stop at sintering. We utilize Hot Isostatic Pressing (H.I.P.). By subjecting the sintered part to simultaneous high temperature and equal gas pressure from all directions, we effectively "squeeze" out any remaining internal voids.
This is the exact same process used for turbine blades in jet engines. If it's safe enough for a Boeing 787 at 30,000 feet, it's the minimum level of safety I accept for our jewelry.
2.5. Quality control: how density is verified
Aerospace-grade MIM parts are not assumed dense; they are measured. Our process uses Archimedes principle testing and, for critical batches, computed tomography to confirm density above 99.2% of theoretical maximum. The same certification logic applies to body jewelry: a mill certificate should state the alloy, the process, and the measured density, not just the finish.
The comparison that matters is not MIM versus casting as marketing terms, but void fraction as a measured number. A cast barbell that looks identical to a MIM barbell can contain 5% internal porosity, invisible to the eye and to a standard loupe. That porosity is where corrosion can initiate and where bacteria can hide. Density certification closes the gap between appearance and structure.